As the biomedical, semiconductor and microelectronics industries continue to evolve, cleanliness control standards for production environments within the healthcare sector keep rising. Conventional protective gloves are prone to particle shedding and high ionic residues, which makes them unable to meet the requirements of high-class cleanrooms.
KINGFA Medical clean-room nitrile gloves are produced with a multi-stage ultrapure water rinsing process. Particle count, ionic content, total non-volatile residue (TNVR), as well as silicone, amide and DOP levels are stringently controlled. Featuring low particle generation, low extractables and chemical resistance, these gloves serve as the mainstream hand protection solution for high-cleanliness environments.
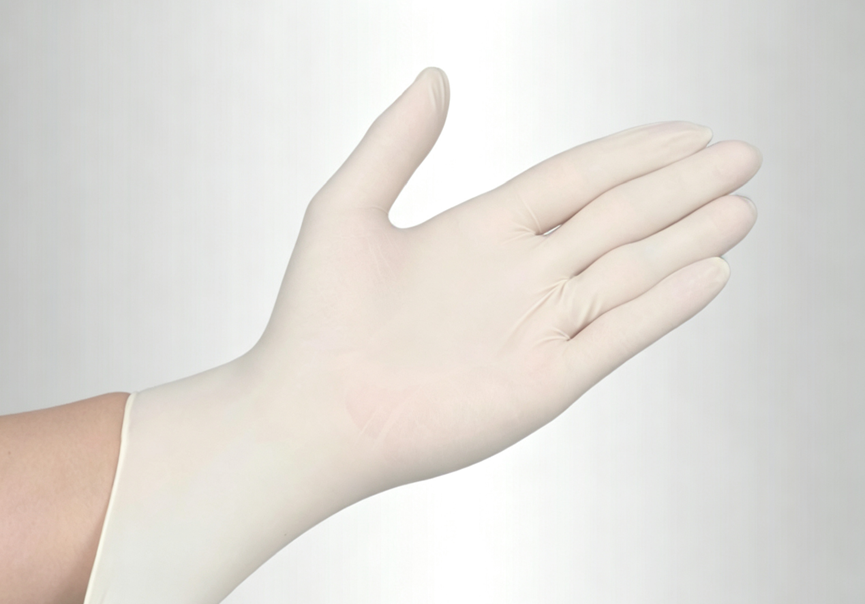
Core Application Scenarios of Clean-room Nitrile Gloves
1. Biomedical and Pharmaceutical Industry
Processes including sterile formulation production, biological agent processing, cell culture, quality inspection and laboratory testing demand extremely high environmental cleanliness. Clean-room nitrile gloves significantly reduce risks of particle shedding and microbial contamination, preventing active pharmaceutical ingredients, finished medicines and test samples from contamination. They preserve drug purity and the integrity of test specimens, and are widely used in compounding, filling, inspection and other procedures.
2. Semiconductor and Precision Electronics Manufacturing
Chips, wafers, PCB circuit boards and precision components are highly sensitive to ionic contamination and surface scratches. Ions extracted from ordinary gloves may corrode circuits, and fine shed particles can cause micro-defects on components. With low ionic content and low extractables, cleanroom-grade nitrile gloves are suitable for wafer transfer, component assembly, precision inspection and other processes to improve the yield rate of electronic products.
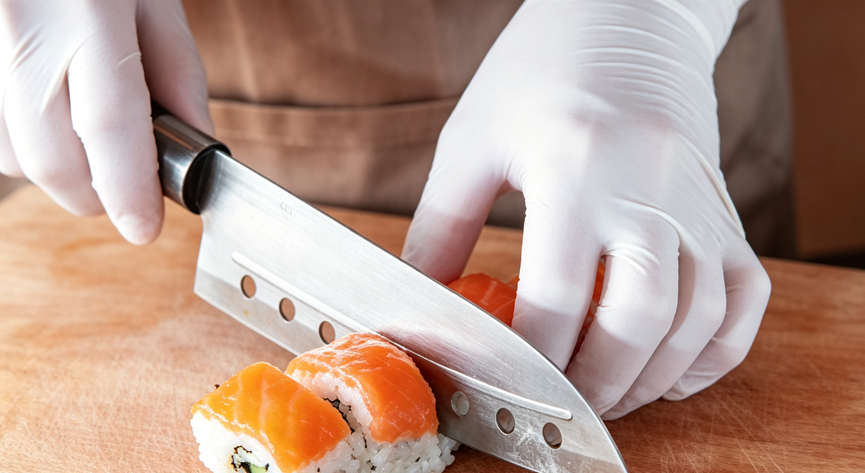
3. High-standard Food Production and Processing
High-end and sterile food processing environments require prevention of cross-contamination introduced by operators. Clean-room nitrile gloves meet requirements for food contact use and can resist food oils and mild detergents. Anti-slip texture on fingertips ensures stable grip during operation. They are applicable to food dispensing, packaging, precision processing and other workstations.
4. Research and Analytical Laboratories
In physical and chemical laboratories, material laboratories and analytical testing laboratories, tasks such as pipetting, sample pre-treatment and precision instrument operation require protection against contact with diluted reagents and solvents. Meanwhile, it is critical to prevent impurities from gloves from entering samples and causing experimental errors. Clean-room nitrile gloves combine protective performance and fingertip sensitivity to accommodate various delicate laboratory operations.
How to Select Suitable Cleanroom Nitrile Gloves
Cuff Length Selection: The product is available in a standard 9-inch version and a 12-inch extended cuff version. When your arm needs to extend into the clean working area, the 12-inch extended cuff model is recommended. It provides a better seal over the cuffs of clean-room garments.
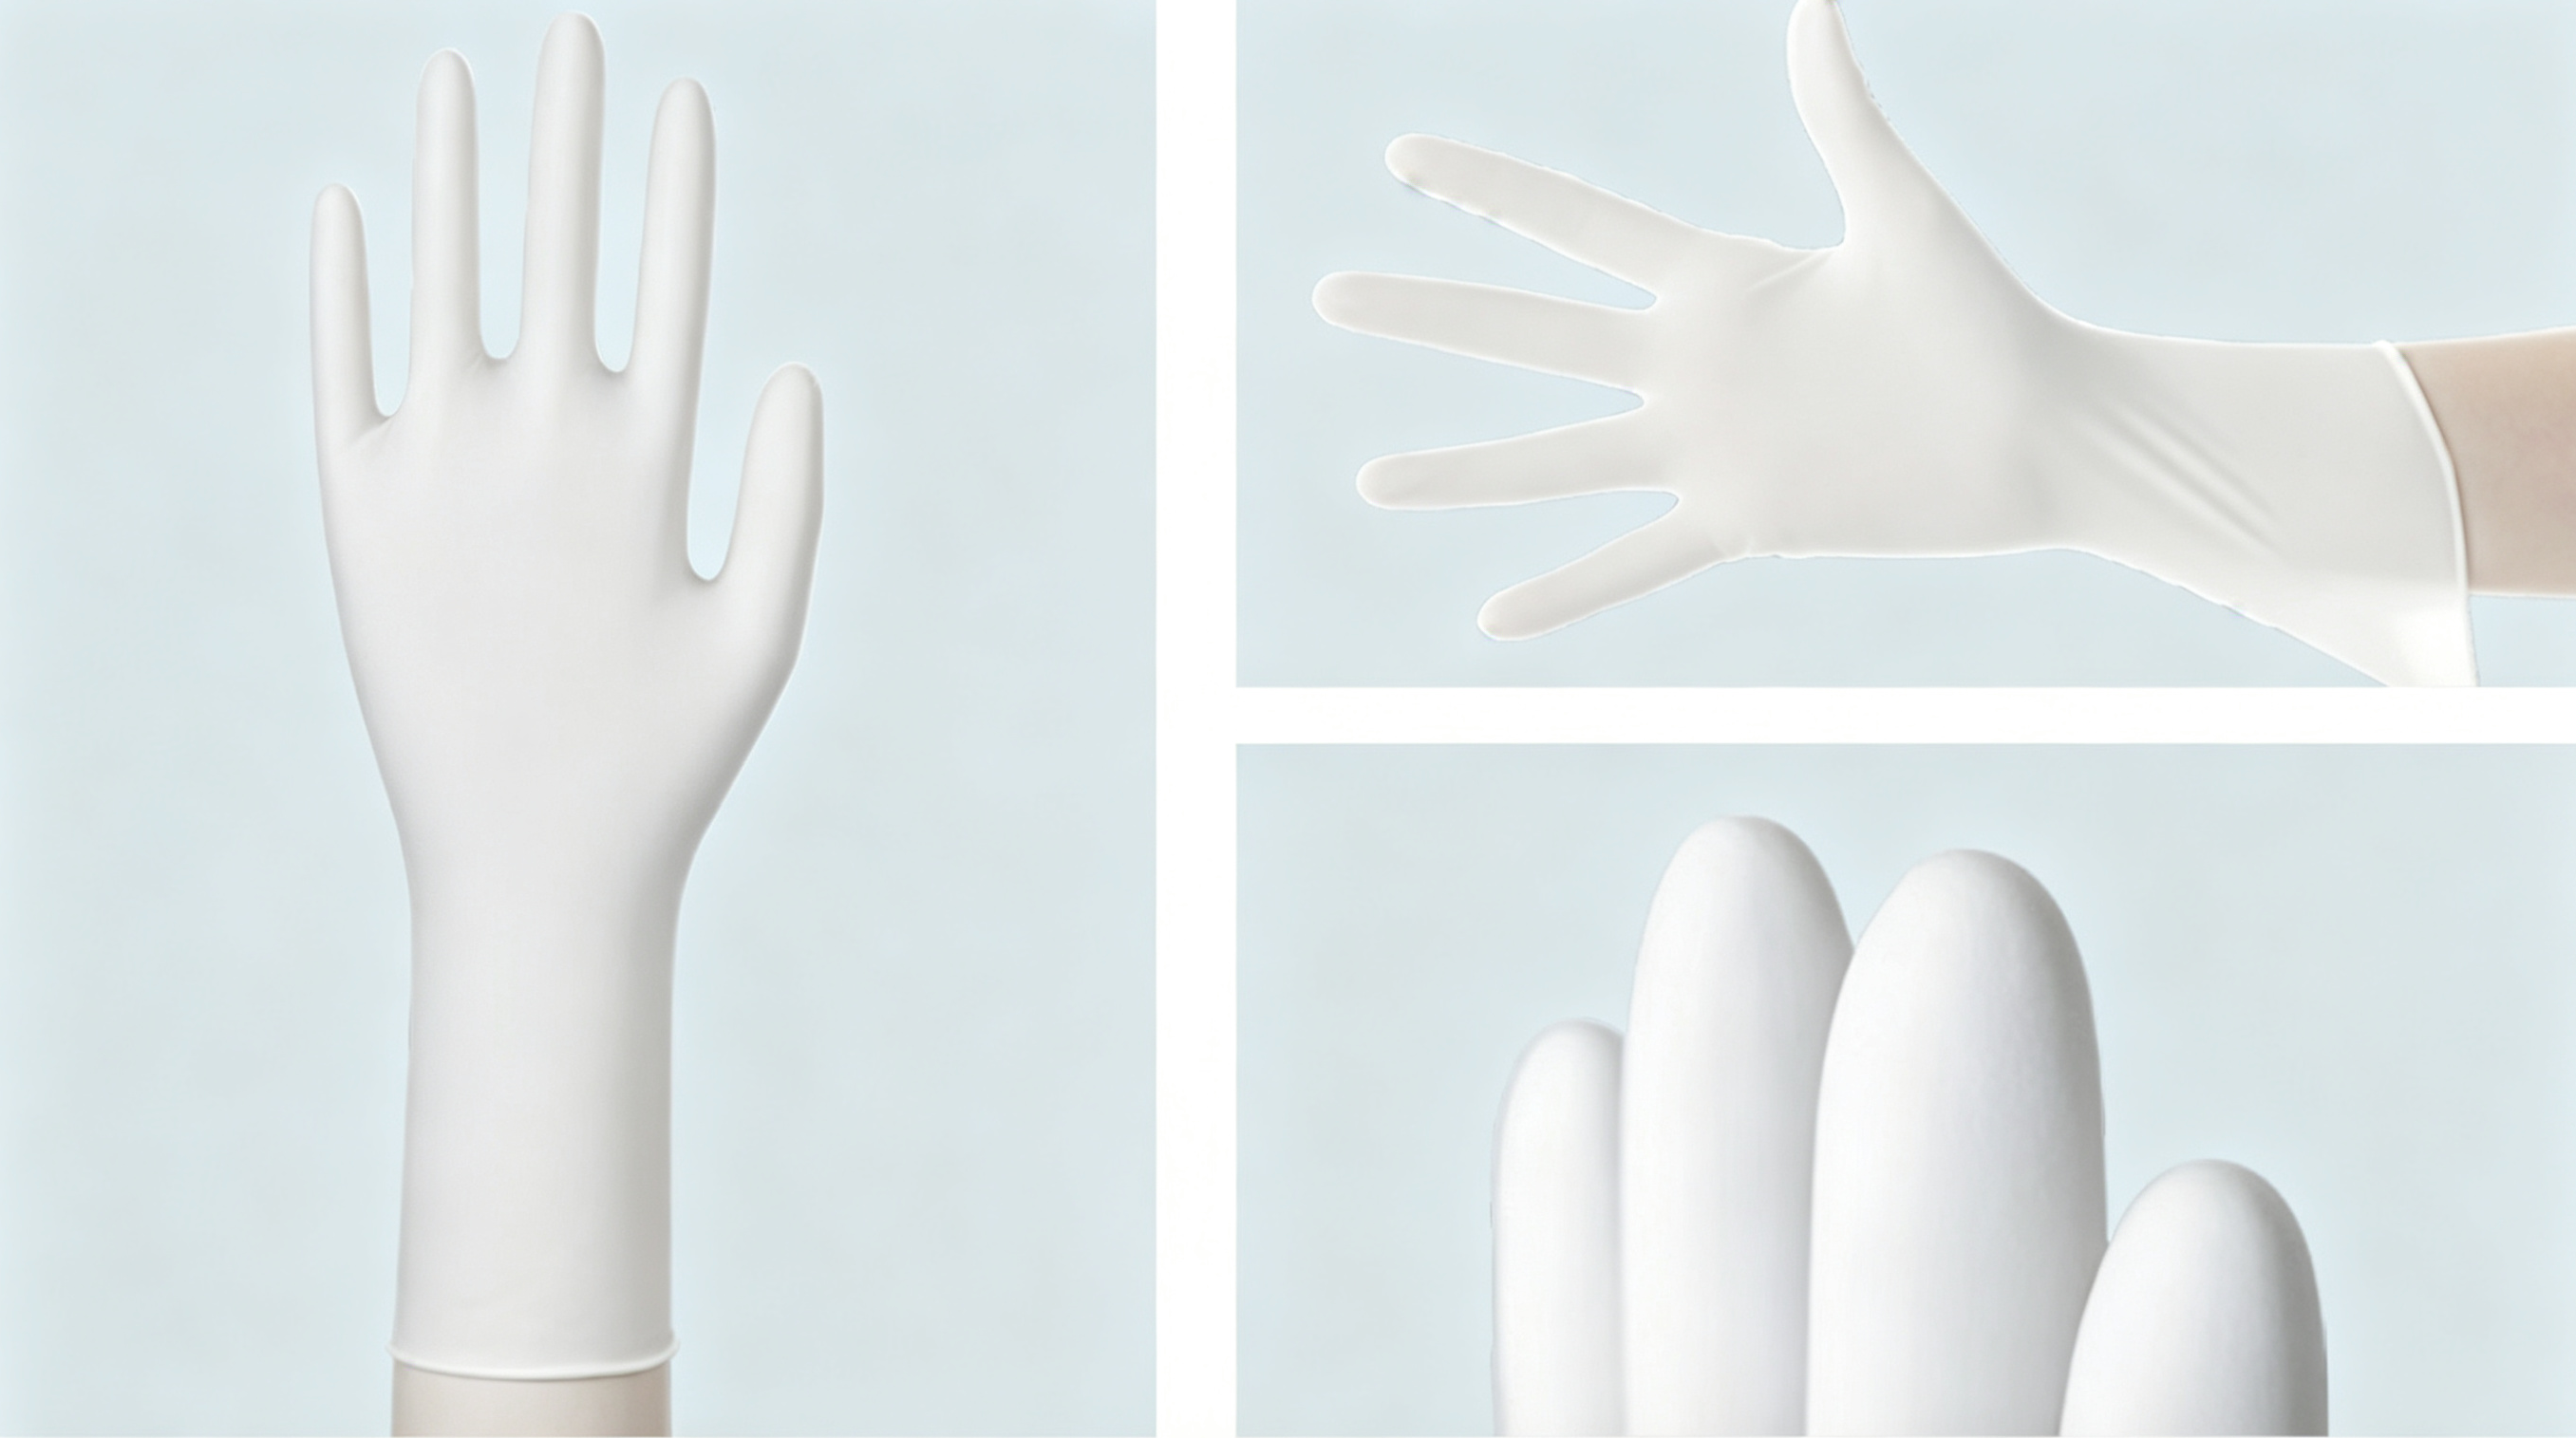
Thickness Trade-off: Heavier-weight gloves deliver superior wear and tear resistance and tear strength. Thinner gloves offer enhanced fingertip sensitivity, ideal for delicate operations.
Advantages of KINGFA Medical Cleanroom Nitrile Gloves
- Ultrapure Water Rinsing Process
Multi-stage ultrapure water washing to strictly control particulates, extractables and ionic residues.
- Wide Range of Specifications
Available in standard 9-inch and 12-inch extended cuff versions with multiple weight options, balancing dexterity and durability.
- Superior Wearing Comfort
Ergonomic design for a snug hand fit. Anti-slip fingertip texture delivers excellent tactility for delicate operations.
- Multi-layer Quality Inspection and Testing
Pinhole, visual and mechanical property tests are carried out. The status of each bath tank on the production line is monitored in real time. Test items include water tightness test (ASTM D5151), physical property test (ASTM D412), and particulate residue test (ASTM D6124).


